All Rights Reserved. Guangu by Guangu Technology (Suzhou) Co., Ltd. | www.jsguangu.com
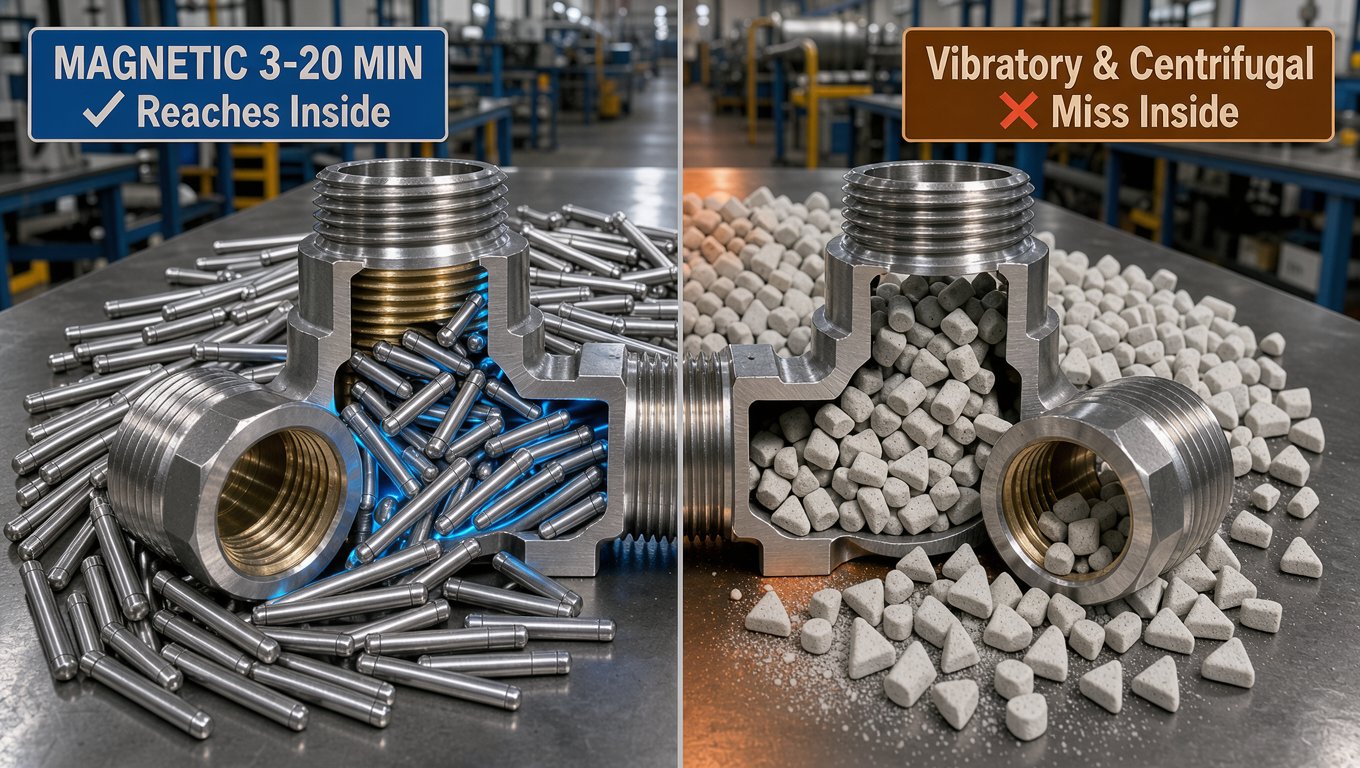
Answer: magnetic pin finishing & deburring of small metals. Magnetic pin deburring of in the package for 3-20min will not produce any warping, pitting or edge rounding or deformation. Vibrator and centrifugal cannot reach deep blind holes or deep internal holes since the media bridge across the holes, and simple hand tools cannot reach deep holes. Deburring through holes is the easiest way to keep the small metal-free. Where is the internal hole: where is the internal hole in the ISO9001 card manufacturer of the magnetic sieve base.
TABLE OF CONTENTS
1. Why Is Internal Deburring the Most Difficult? 2. Ways to Remove Burrs: 3. 4 Essentials 4. Round Vs Square 5. SOLUTION: Two Solutions 6. Benefits of Choosing Guangu 7. Brief Comparison 8. Applications & 4-Step 9. FAQ 10. Final Words
Surface burrs that are easy to dispose of – a bowl or disc will get rid of these. Internal burrs are another story:
The key is allowing the flow to go into a hole, not just around a hole.
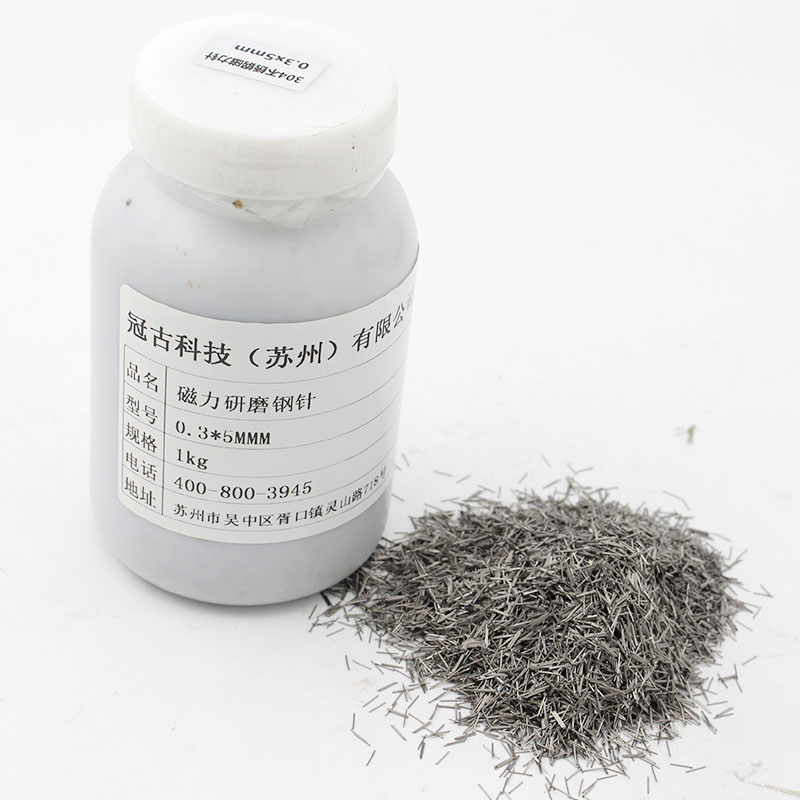
RPM high frequency rotating magnetic field excites 0.3-1.0mm diameter stainless steel pins. – Pins form liquid spray brush that are inhaled into blind holes, threads and cavities hundreds of times per second- deburring media will never touch!
1. Charge parts + pin align (0.3mm M1-M3, 0.5-0.8mm 3-8mm holes, 1.0mm cavities) + water + agent (1:50).
2. Activate: Alternating field pulls pins into the hole and moves with a spiral pattern over the threads.
3. Finish: Burr and oxide are removed in 3-20 mins. – enhancement of the surface roughness can be checked against the NIST surface metrology.
Internal geometry analysis of deburring and surface finishing, magnetic finishing is favored while the surface finishing articles ensure you vibratory media cannot get into blind features.
Vibratory tumbling For very complex internal shapes. Eccentric motor causes bowl of heavy ceramic or plastic media to shake. Media bridges over holes less than 8mm and is unable to reach blind cavities. Cycle 1-6 hours, poor internal access.
Centrifugal Disc/Barrel: 15-20G aggressive cut 5-30minutes – media will not follow threads; high impact scratching kills the fine internal edges.
Guangu metal polishing machine: Metal Polishing, Deburring, De-oxidize and Inner Hole Polishing for gold, silver, brass, copper, aluminum,304 stainless, titanium and zinc alloy–low pin consumption–high hardness–long-lasting high durability, for threads and cavities.
1. Hole Diameter & Thread Size Magnetic holes sit in M1.0 thread hole (black) Through-hole >0.8mm vibratory Large hole through the part >8mm connects to large embossed registration holes. Match the diameter of your M1.0 thread with pitch of thread: Fine=0.3mm, Coarse=0.6-1.0mm
2. Depth & Blind vs. Through – Media stored in a hole or cavity: The only media pins are trapped and can not be retracted: through hole media must be unseated to access the cavity. Blind hole magnetic pins can not be penetrated.
3. Edge & Tolerance Sensitivity – Sharp Thread, magnetic nonimpacting (no change in part size). Vibratory or centrifugal completes. The thread crest and provides damage on the tap.
4. Certifications & Material Coverage Magnetic Guangu units are CE / RoHS / MSDS approved (metals) ISO 9001:2015 certified. Use same system for brass fittings, aluminum manifolds and stainless valves. See options in our shop.
ROUND Φ350-Φ500mm (8-18kg)
Small interior details, subtle features M1 – M6 threads, 1-6mm blind holes, watch screws, dental implants, electronic pins. Make the slowest of turns with a little to no thread engagement. SQUARE + TRANSLATION (20-80kg)
Extra deep internal cavity, for example in manifolds, valve bodies, hydraulics blocks, long couplers. Clear translation dies dead area for deep cavity.
Rule: Thread: Less than M6 / >6mm Round. Openings: >30mm deep holes/ More than 15kg Square.
Leave us to do what nobody else is doing: Magnetic polisher for internal deburring work.
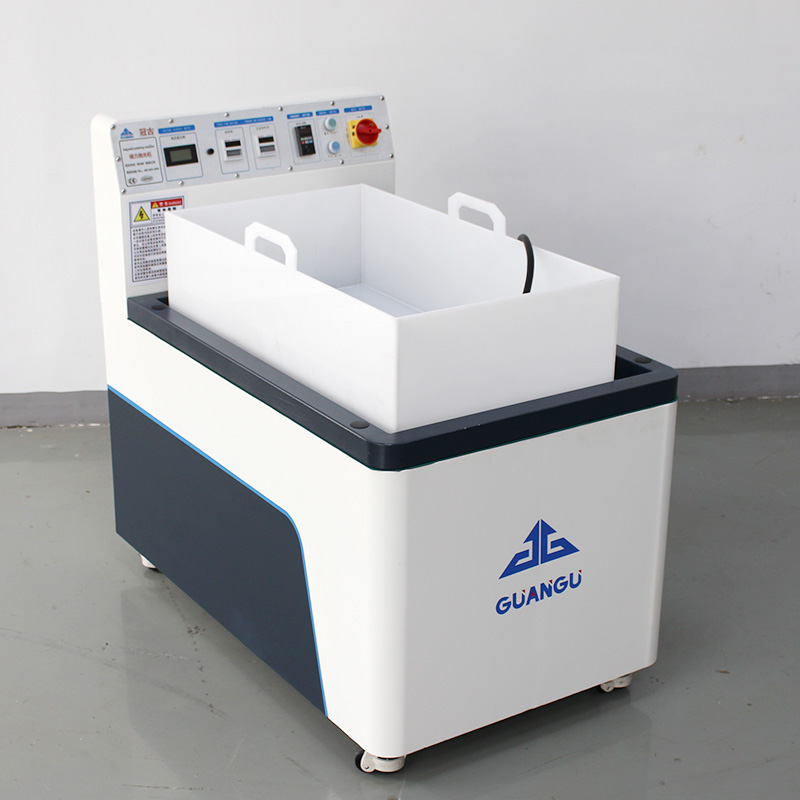
Brass fittings m2-m4 threads, copper terminal cross thread bores, aluminium fuel nozzle 2mm dia holes-each vibratory leave burrs, each hand tool too often leave burrs behind. Meet our Magnetic Polishing Machine GG8520 (Φ350mm round, 8-10kg, 2.2kw×1, 168kg, 640×520×1088mm)-the thread-and-hole machine. $2,500 (sale)Φ350 round bucket +0.3mm pin nozzle-m1.5 threaded leads and 1.5mm blind hole in 3-8 min-each thread crest remains clearly crisp, every cavity free of burrs. Positive/Negative rotation, footprint suited to cell-side.
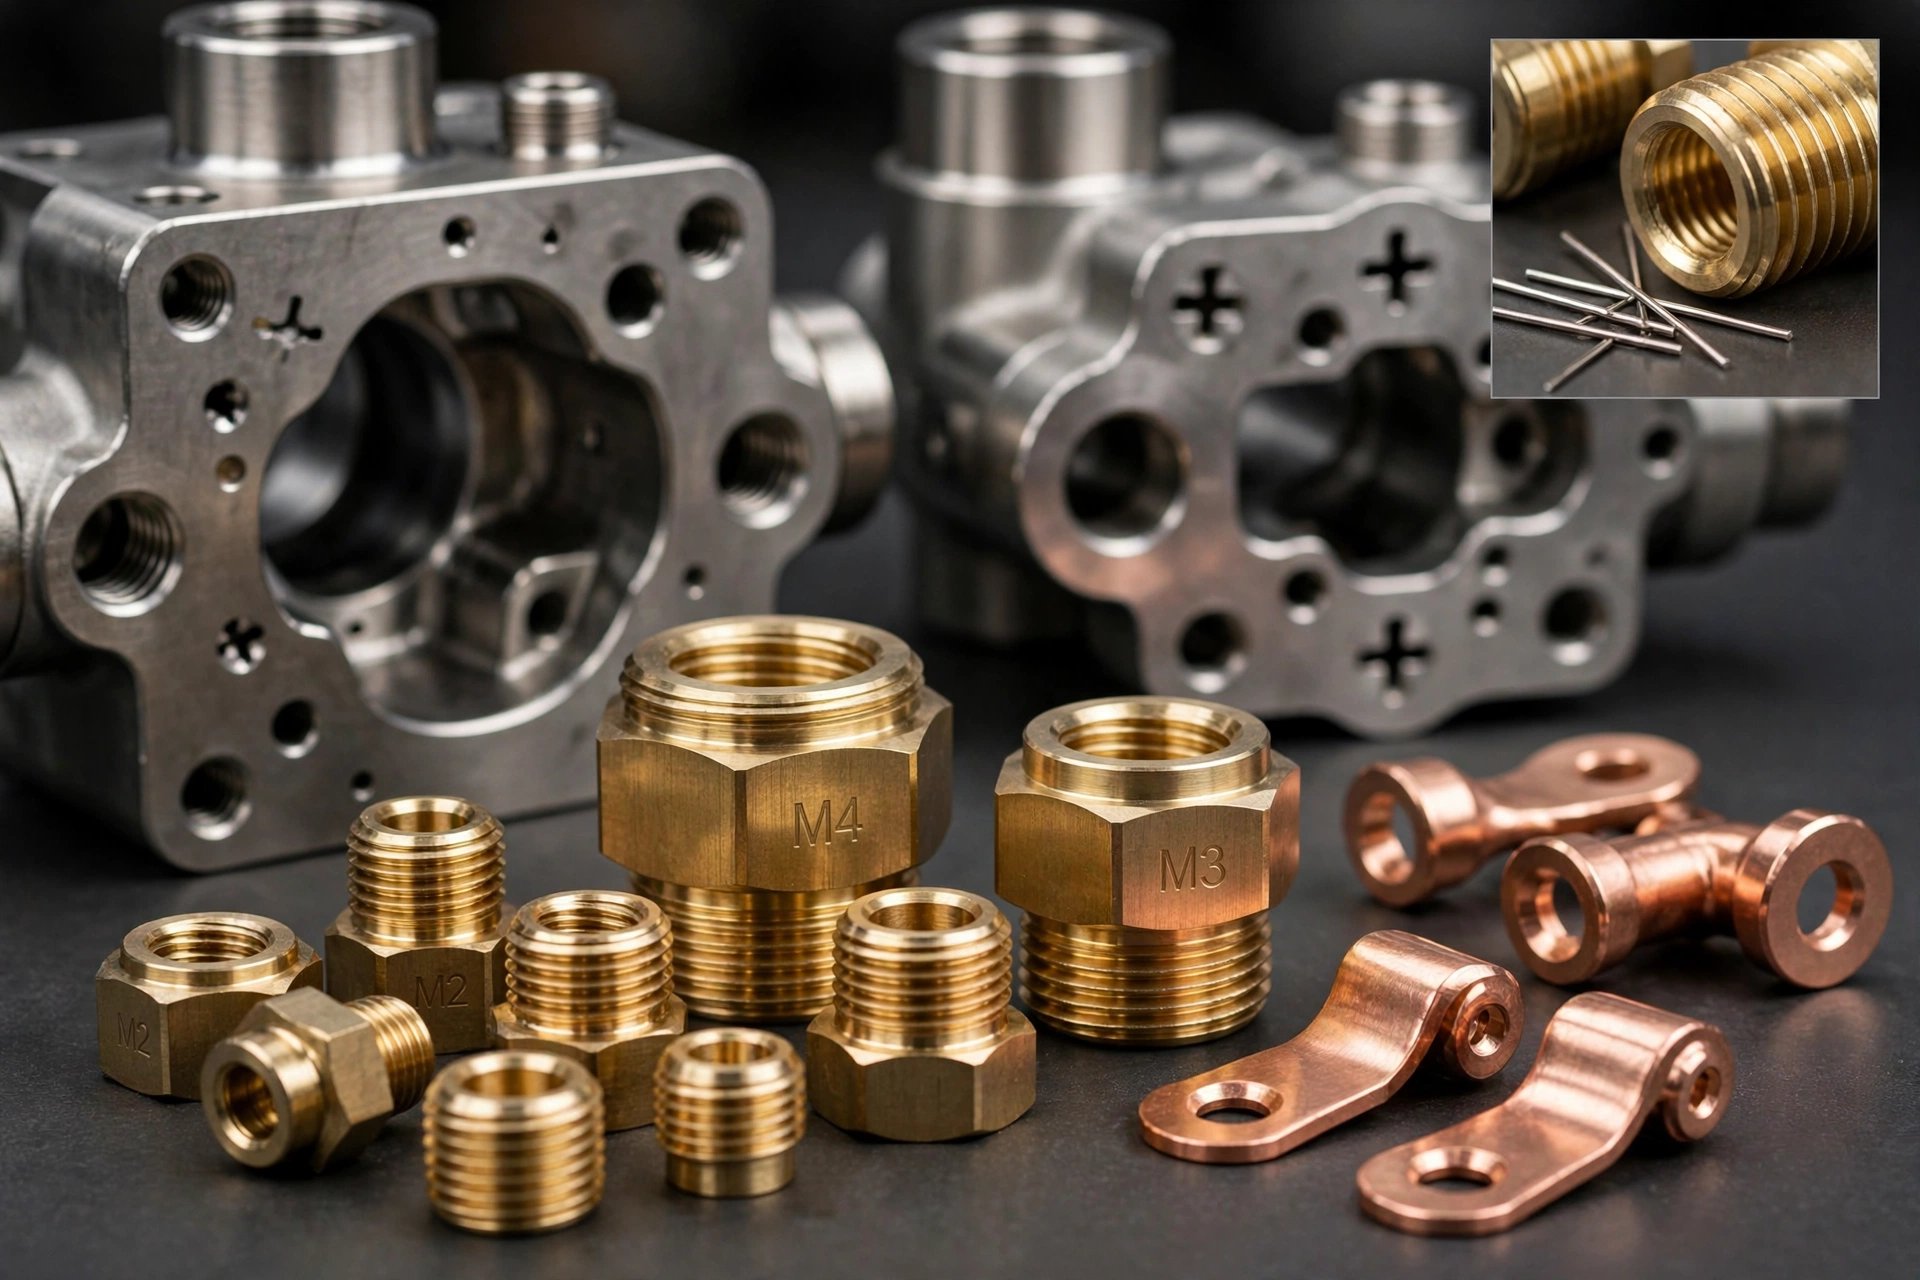
Think 304 stainless manifolds with 40mm deep cavities, hydraulic valve bodies with cross drilled holes, automotive housings vibratory media bridges, centrifugal crushes edges Our Magnetic Polishing Machine GG8850 (900×500mm square + Translation, 20-30kg, 4.0kW×1, 288kg, 1200×720×1088mm) the cavity specialist – $6,000 900×500mm translational trough with 0.5-0.8mm pins – deburrs deep cavities and blind cross-holes in 5-15 minutes – what hand deburring takes hours – without missing a bore. Positive/Negative rotation + translation – no dead zones – low noise.
Not sure what fits your threads/holes? Ship us 1-2kg of pieces with worst internal burrs, we will video up/down test on magnetic alternative and quantify thread quality. Message us via our shop. Here are only two, the full range at Guangu Technology fits all 8 models (8-80kg).
You choose a system that performs deburring action on internal as well as external.
Standard certification GB/T 19001-2016 / ISO 9001:2015 – No. 30625Q0093R0C
Scope Assembly and Sales of automated mechanical equipment – Magnetic polishing machine Magne Tune the internal hole deburring qualified for all metals
Warranty Date Mar 03, 2025 – Mar 02, 2028
Verification national accreditation CNAS (C241-M) & IAF MLA, but the English version of CNAS database and www.cnca.gov.cn.
Standards CE, ISO 9001, RoHS, MSDS + Video Inspection + Test Report
Furthermore: Trademark of GUANGU™ Trademark: 51870579 Classification: 7 – Polishing Machinery 2021-2031 CNIPA
Visit the official ISO 9001 page and CNAS English database.
| ITEM | DETAILS |
| Standard certification | GB/T 19001-2016 / ISO 9001:2015 – No. 30625Q0093R0C |
| Scope | Assembly and Sales of automated mechanical equipment – Magnetic polishing machine Magne Tune the internal hole deburring qualified for all metals |
| Warranty Date | Mar 03, 2025 – Mar 02, 2028 |
| Verification | national accreditation CNAS (C241-M) & IAF MLA, but the English version of CNAS database and www.cnca.gov.cn |
| Standards | CE, ISO 9001, RoHS, MSDS + Video Inspection + Test Report |
| Furthermore: Trademark | GUANGU™ Trademark: 51870579 Classification: 7 – Polishing Machinery 2021-2031 CNIPA |
| Feature | GG8520 Magnetic (Threads) | GG8850 Magnetic (Cavities) | Vibratory | Centrifugal |
| Cycle Time | 3-8 min | 5-15 min | 1-6 hours | 5-30 min |
| Key | Φ350mm round buckets | 900×500mm + translation | large bowl | high-speed disc |
| M1-M6 Thread | Excellent – 0.3mm pins | Good – 0.5mm pins | Cannot quite get | Damages crests |
| Blind Hole <6mm | Good – flow pins | Good – multi station | No – bridges | No – bound |
| Deep Cavity >30mm | Limited – small bucket | Good – translational | Poor | Moderate |
1. Prep: clean, inspect, pin diameter (0.3mm M1-M3, 0.6mm M4+ 0.8mm cavity), grounding?
2. Maximum: Components + pins + water 2-4cm beyond + agent 1:50 + timer 3-20mins (3-8mins threads, 8-15mins cavities).
3. Run: Cover, fire, water <50°C, relax 10-15min every 2h.
4. END: Stop, magnetic separation, wash, dry, thread-gage check, cleans.
Q1: Can magnetic deburr M1.0 threads without damage?
Yes – GG8520 0.3mm pins at 3-5 min deburrs M1.0-M3 thread holding crest geometry – shown by thread gauge – but vibratory rounds the crest.
Q2: How deep does it go?
Pin forming within blind holes to a depth of 40mm maximum (GG8850 with translation); for deeper holes move the pin translationally – available from mass finishing literature.
Q3: Aluminum vs. Stainless threads?
The two work – aluminum 3-8 min; stainless 0.6-1.0 mm 10-15 min – can be determined with the aid of the NIST roughness standards.
Q4: How to verify whether suppliers’ claims are true?
Proceed to check ISO 9001 (No.30625Q0093R0C from CNAS English site or ISO 9001 page). Guangu provide onsite and webcam inspection.
The burrs inside the blind hole, cavity, thread, only one principle is flow inside- magnetic pin finishing (Vibratory finishing and Centrifugal finishing are surface only) The GG8520 is suitable for fine thread; The GG8850 is suitable for deep cavity; Both models are ISO9001:2015 (30625Q0093R0C) under, with GUANGU™Trademark, worldwide support.
Contact Information:
No account yet?
Create an Account
 Product Category – Mirror polishing machine
 Product Category – Magnetic Pin